WEBER-Technology

What you should know about modern screwdriving systems

These are the areas of application for modern screwdriving systems

Modern screwdriving systems are used in the electrical, timber and aviation industries as well as in the e-mobility sector, in mechanical engineering, telecommunications and in household appliances and medical devices. The automotive industry and car body construction are the largest area of application for WEBER.

https://www.weber-online.com/schraubtechnik-fuer-automotive-und-karosseriebau/

Maximum reliability and permanent connections or detachable individual parts are key elements in the manufacturing of car bodies. This requires screwdriving systems from professionals, because the materials requirements are high. The required fasteners have to be lightweight, strong and cost saving. This used to mean: welding. Modern production is different, though. Professionals today use automated screwdriving systems – highly flexible, very reliable and with an error rate that moves towards zero. In addition, the products are easier to dismantle and recycle at the end of their life cycle. How does it all work? Our guide offers insights.
Basics of modern screwdriving technology

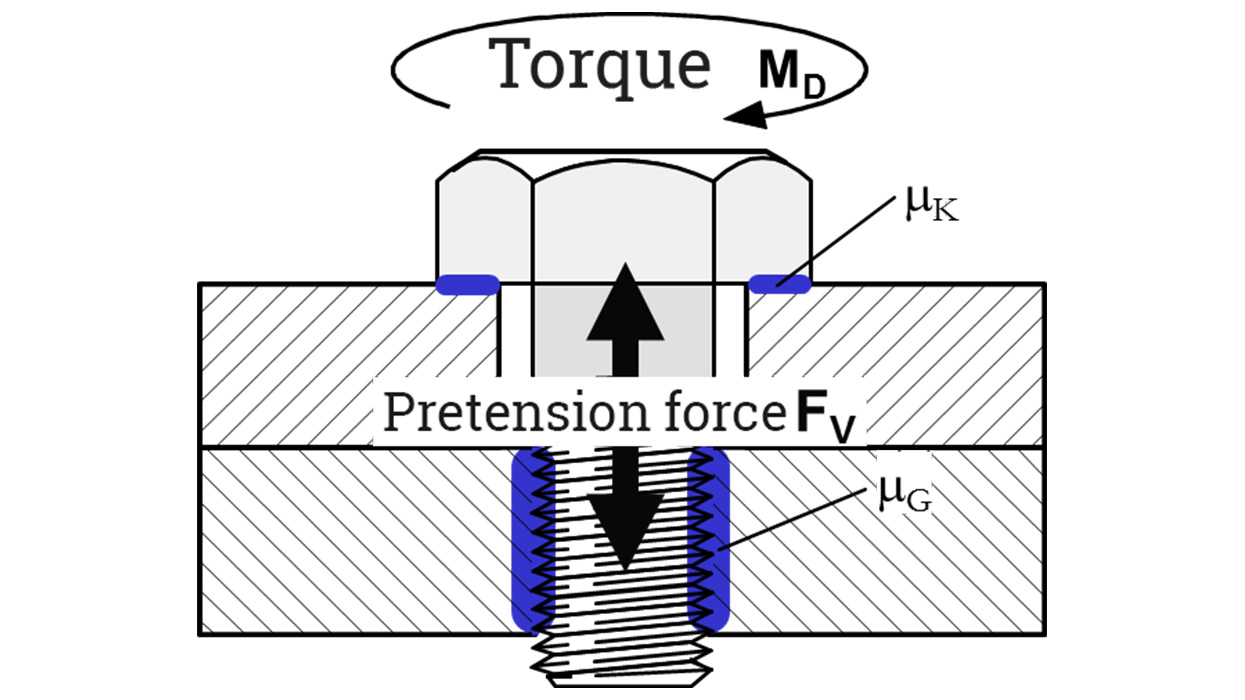
Screwdriving-torque-preload-force-WEBER.

Reliable assembly processes are the core competence of modern screwdriving systems. Industrial customers want high-quality processing of fasteners for their expensive goods. With the highest quality benchmarks and optimised cycle times, screwdriving systems ensure thorough, reliable and fast joining of individual parts. Advance test parameters help to avoid product recalls. The top priority of a screw connection is to join two or more components – in the correct way: In the end, they have to act as a single component. The required clamping or pre-tension force has to be generated accurately and reproductibly. Different screw connections require different pre-tension forces. These are determined in advance so that all parameters for the screwdriving systems are correct. The objective here is to apply the calculated pre-tension force as accurately as possible, because precision work results in a reduction of materials and costs.

4 modern screwdriving proccesses

Here, we give you an overview of the 4 most common screwdriving processes:

  • Screwdriving to depth
  • Torque-controlled screwdriving
  • Angle-controlled screwdriving
  • Yield-strength-controlled screwdriving (gradient screwdriving method)
Graphic screwdriving into depth WEBER

Screwdriving to depth

For screwdriving to depth, on timber connections for example, the head of the screw is countersunk.

Diagram of a screwdriving curve for screwdriving to depth

Rudolf, 1992

Graphic torque controlled screwdriving WEBER

Torque-controlled screwdriving

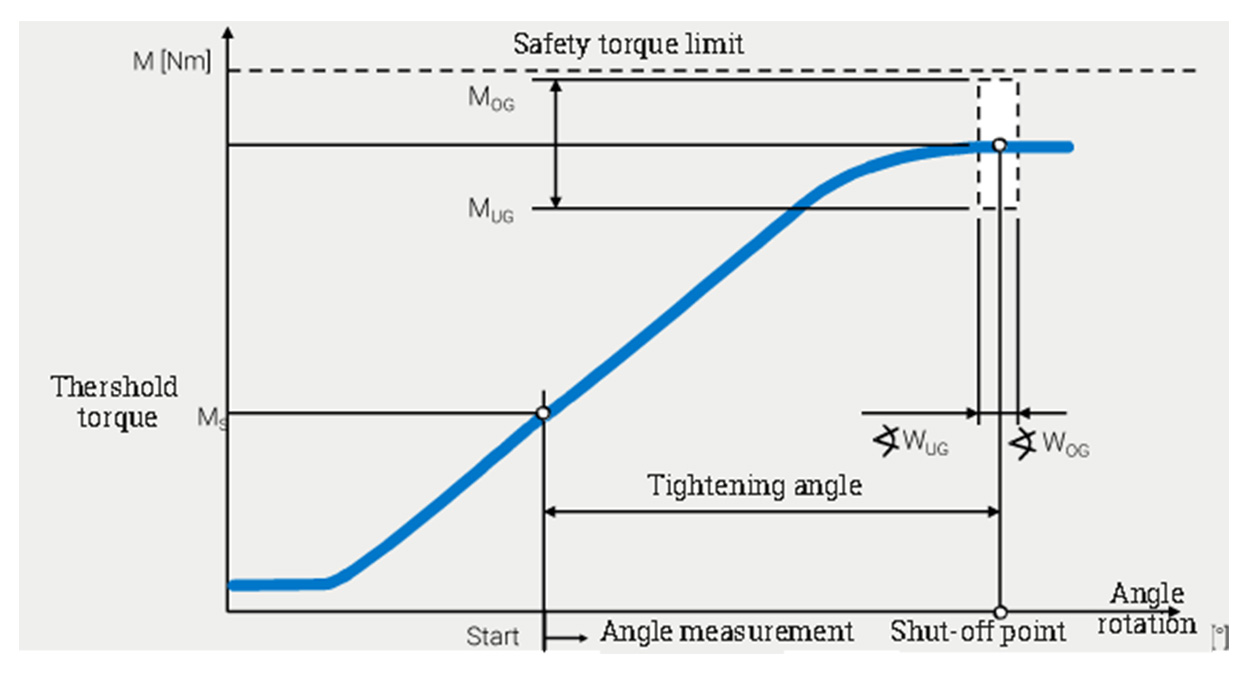
The objective of torque-controlled screwdriving is to tighten the screw to a pre-tension force below the yield point. The screw is tightened until a preset torque has been reached. Then the screwdriving unit is switched off. For most of our customers’ applications, we use torque-controlled screwdriving.

Diagram of a screwdriving curve for screwdriving to torque

Rudolf, 1992

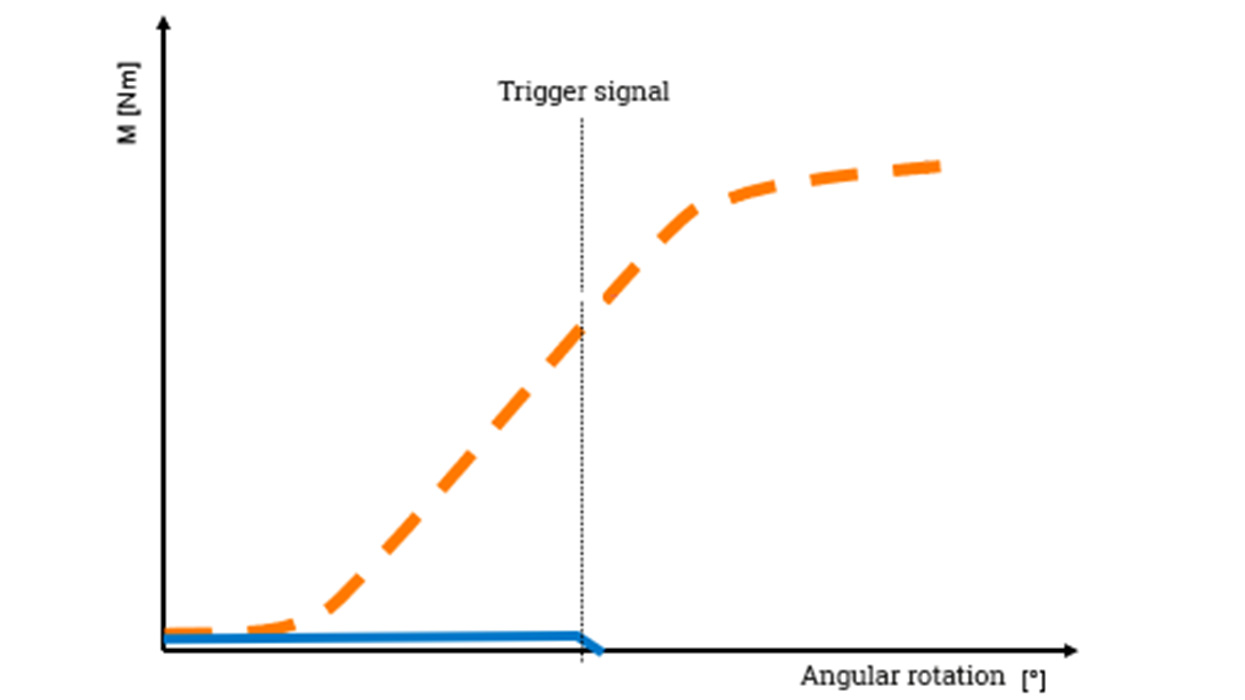
Angle screwdriving WEBER

Angle-controlled screwdriving

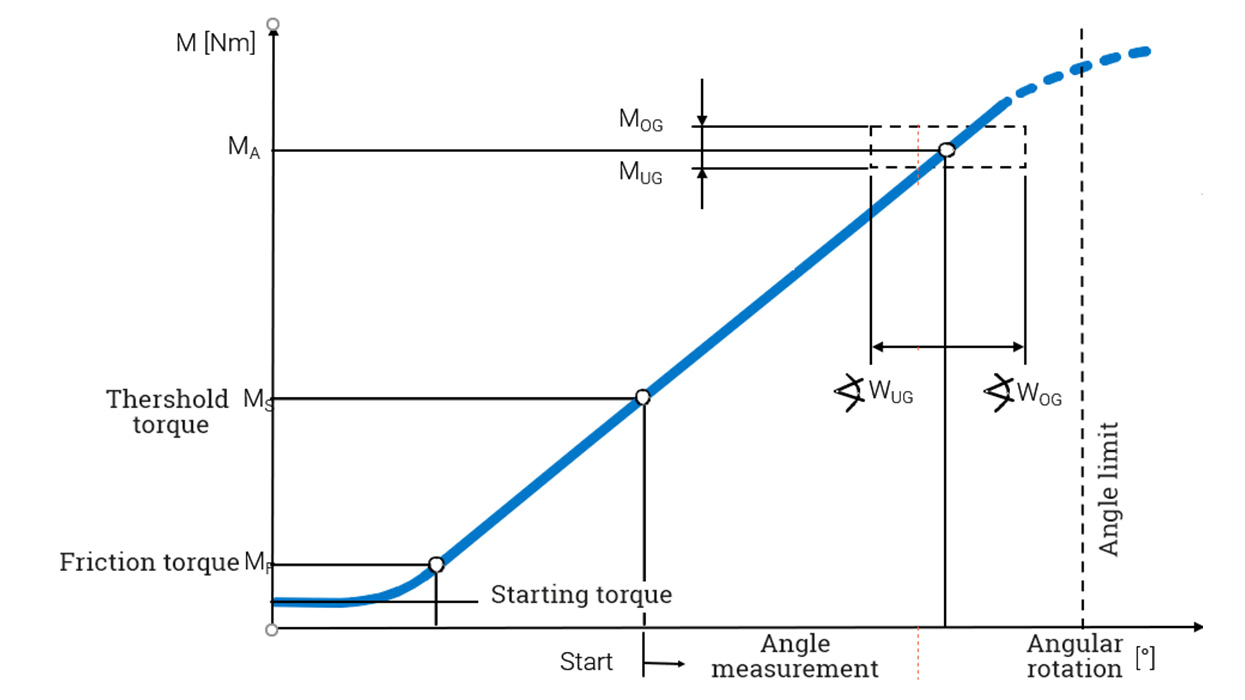
For angle-controlled screwdriving, the screw is tightened until it reaches the plastic range. The screwdriving process starts with tightening of the screw until the pre-defined threshold torque (M) has been reached. This is when the angle measurement starts. The screwdriving unit is switched off when the pre-defined rotation angle has been reached. All calculations concerning angle-controlled screwdriving have to account for any – including extreme – weather conditions, temperature fluctuations and signs of wear in advance

Diagram of a screwdriving curve for screwdriving to rotation angle

Rudolf, 1992

Graphic-gradient-method-WEBER

Yield-point-controlled screwdriving (gradient screwdriving method)

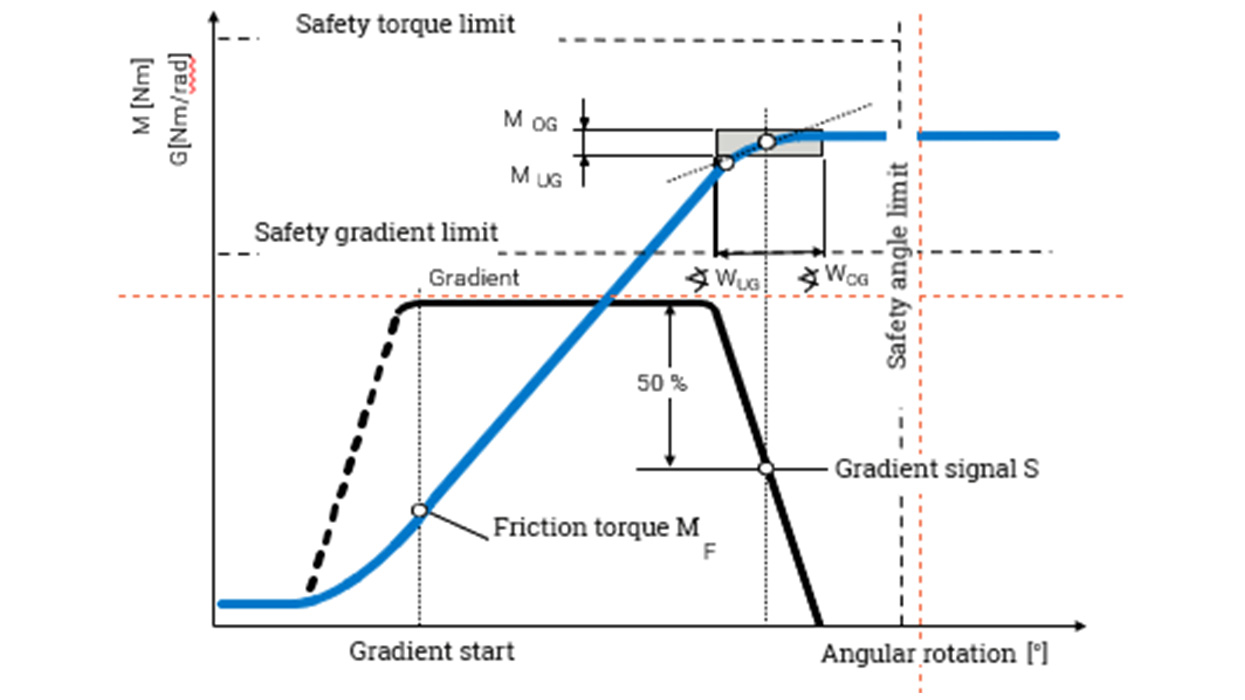
The objective of the gradient screwdriving method is to tighten the screw to just before the yield point is reached. The switch-off here occurs based on a falling gradient, not on a torque or angle. The controller continuously calculates the gradient from the torque increase per rotation angle. The screwdriving process stops when the gradient falls by a pre-defined percentage of the maximum. This screwdriving process is still in its early days. This process could only be developed with powerful screwdriving process controllers with reaction times in the millisecond range. The advantage of this method is the highly precise shut-off just before the yield point is reached. This eliminates friction in the thread as much as possible. The drawback is that the shut-off torque can have a large spread depending on the application. This often poses a problem for traditional quality assurance.

Diagram of a screwdriving curve for screwdriving using the gradient screwdriving method

Rudolf, 1992

Conclusion

Selecting the best screwdriving method is essential for the result. We are always working on improving our process quality and are always available for questions on screwdriving systems.

https://www.weber-online.com/stationaerschrauber/

FAQ ON SCREWDRIVING SYSTEMS

Welche Antriebstechniken verwendet man eigentlich heute in der Schraubtechnik?

Aufgrund der derzeitig in der Industrie vorherrschenden Anforderungen hat sich der EC-Servo-Motor in der modernen Schraubtechnik durchgesetzt. In Hinblick auf Langlebigkeit und Genauigkeit stellt er die beste Lösung innerhalb aktueller Antriebstechniken dar.

Was ist unter Vakuum Schraubtechnik zu verstehen?

In zahlreichen Einsatzgebieten der automatisierten Schraubtechnik gibt es Schrauborte, die sehr schwer zu erreichen sind. Hier kommt die Vakuum-Schraubtechnik zum Einsatz. Dabei wird die Schraube über ein Saugrohr aufgenommen. In diesem Saugrohr wird ein Unterdruck erzeugt. Eine auf den Schraubfall angepasste Einschraubgarnitur mit Saugrohr sorgt dafür, dass das Verbindungselement prozesssicher genau an der richtigen, wenn auch schwer zugänglichen Stelle platziert wird.

Wie funktioniert der Schwenkarm bei der Schraubtechnik?

Der Schwenkarm ist ein wichtiges Funktionselement innerhalb des Schraubtechnik-Prozesses. Im Schwenkarm wird eine Schraube Richtung Schraubkopf geblasen. Der Schraubendreher richtet den Schwenkarm zur Seite in die richtige Position. Schon während des Eindrehens der ersten Schraube schießt bereits die nächste in den Schwenkarm ein. Sobald die Schraube platziert und eingeschraubt ist, wird der Schwenkarm freigegeben. So kann er sich in seine ursprüngliche Position zurückbegeben und der Prozess startet von Neuem.

Der Schwenkarm ist also ein äußerst zeitsparendes Element der modernen Schraubtechnik.

Schwenkarmprinzip Automatische Zufuehrung WEBER
Schwenkarmprinzip WEBER

Wann verwendet man einen Handschrauber und wann einen Stationärschrauber?

Ein Handschrauber wird manuell von lediglich einer Person betätigt. Handschrauber kommen dann zum Einsatz, wenn die Verschraubung flexibel gestaltet werden soll und die Anzahl der zu verschraubenden Elemente bei 20.000 – 50.000 Stück pro Jahr liegt.

Mehr Informationen zu verschiedenen Handschraubern finden Sie hier: https://www.weber-online.com/handschrauber/.

Bei der nicht-manuellen Variante Stationärschrauber ist die Schraubeinheit beziehungsweise -spindel an einen Roboter gekoppelt. Stationärschrauber kommen bei hohen Stückzahlen (> 50.000 Verbindungselemente/Jahr) und schnellen Takteinheiten zum Einsatz. Im Gegensatz zu Handschraubern sind sie prozesssicherer: Mittels der Schraub-Tiefen-Überwachungsfunktion lässt sich genau berechnen, wie tief der Schrauber bereits eingeschraubt hat. Ein schiefes Ansetzen der Schrauben wird ebenso vermieden.

Verschaffen Sie sich hier einen Überblick über unsere Stationärschrauber: https://www.weber-online.com/stationaerschrauber/.

WEBER Schraubautomaten

WEBER Schraubautomaten GmbH is a family-run and innovative company that attaches great importance to the sustainable design of the value chain. The result is high-quality products with maximum process reliability that make production processes more efficient. Your success is our success.

FREE Webinar:
Blind rivet nuts on the rise!

How automation enables reliable threads in thin-walled structures

Modern lightweight constructions are defined by thin materials and, at times, one-sided accessibility. Creating strong and durable threads under these conditions pushes conventional fastening methods to their limits. Blind rivet nut inserting provides robust and reliable threads . Whether in automotive, IT equipment or household appliances, automated processing delivers stable performance and higher productivity.

In this webinar you will learn about:
✅ Key challenges and opportunities
✅ How automation transforms the blind rivet nut into a high-performance inserting solution

Learn why blind rivet nut inserting is the right choice for your assembly process — and how automation can take it to the next level in efficiency, consistency and reliability.

  • 19.11.2026
  • 10:00 & 16:00 (CET)
  • English